A high-volume fixture must meet a production target without introducing datum errors, loading variation, unsafe clamp states, or maintenance delays. By defining the process demand first, then matching the locating, clamping, changeover, inspection, and validation details to it, you can choose a fixture concept that remains reliable across thousands of cycles.
Key takeaways
- Compare takt time with loading and machining time before selecting a fixture.
- Use GD&T to define stable locating points and prevent over-constraint.
- Size clamps for cutting forces while protecting thin or flexible surfaces.
- Qualify repeatability, interchangeability, and traceability before production release.
Start with production demand before choosing the fixture concept
Calculate annual production volume, takt time, batch size, machine availability time, loading time, and required cycle time before selecting a fixture. If demand requires a 90-second takt but loading takes 25 seconds and machining takes 80, one station cannot meet output; add capacity, parallel fixtures, or redesign the operation.
Include tool access, probing, deburring, inspection, cleaning, and removal. A locator that blocks a cutter or probe turns an automated cycle into manual work.
Use the production pattern to narrow the concept:
| Option | Use when | Watch for |
|---|---|---|
| Jig versus fixture plate | Guided drilling versus simple holding | Guidance versus positioning |
| Modular fixture | Parts and batches change | Setup and requalification |
| Dedicated fixture | Stable, high-volume part | Obsolescence |
| Tombstone | Multiple machining faces | Spindle reach and chips |
| Palletised fixture | Fast pallet exchange | Pallet interface |
| Soft jaws | Repeat machined profiles | Jaw boring |
| Magnetic fixture | Flat ferrous parts | Holding force and magnetism |
| Vacuum fixture | Thin, nonferrous parts | Sealing and cutting forces |
| Robotic welding fixture | Repeat welded assemblies | Torch access and spatter |
Pneumatic or hydraulic clamping supports consistent loading, but pressure confirmation, clamp-position sensing, and a machine interlock are essential when clamp loss could eject a part or damage tooling. Make incorrect loading physically difficult with keyed nests, unequal pin spacing, orientation stops, and chip relief; sensors alone can be fooled by chips.
Convert the drawing and GD&T into a locating scheme
A fixture that locates from the largest available face can produce a repeatable wrong part. Start with the functional datum locating surface, hole pattern, and feature relationships that control assembly, then build the datum reference frame defined by ASME Y14.5 rather than inventing a convenient substitute.
1. Identify the primary, secondary, and tertiary datum features on the drawing. Convert each into a physical contact scheme: the primary plane controls three degrees of freedom, the secondary plane controls two, and the tertiary feature controls one under the 3-2-1 locating principle.
Check that the inspection datum matches the assembly datum; changing it transfers error into the feature tolerance.
2. Place locators where the part is stiff and where the functional features are dimensioned from them. Use a round pin for the first hole and a diamond pin or relieved pin for the second. Two full round pins can bind because hole size and position tolerances over-constrain insertion.
3. Read the position, profile tolerance, and surface requirements together. A profile tolerance on a sealing face may demand broad support, while a hole pattern may require pins that locate without forcing the part into nominal position. Add supports along the cutting-load path, not wherever access is easiest.
A locator that touches twice without a deliberate floating or compliant design is a redundant locator and can lift, distort, or shift the part. Account for thermal growth by allowing movement in one controlled direction, especially on large steel fixtures or temperature-sensitive components; otherwise coolant temperature becomes an unrecorded locating variable.
Size clamps for cutting forces without deforming the part
Calculate clamp force from the cutting force and torque at the tool-workpiece interface, then resolve those loads through the workpiece to the locators.
For sliding, use F = (cutting force × lever arm + torque) / (friction × reaction arm), then multiply the result by a stated safety factor for interrupted cuts, tool engagement, and pressure loss. Check overturning moment separately.
- Make the clamp push the part into its locating elements, not away from them.
- Check local bearing stress and elastic deflection at every contact; excessive clamp pressure on a thin wall can create more error than cutting.
- Place the clamp over a stiff load path, with sufficient contact area and clearance for the cutter, probe, chips, and part removal.
- Use clamp pressure confirmation and a machine interlock when a leaking circuit or incomplete actuation could eject the part or damage tooling.
| Method | Strength | Main limitation or use |
|---|---|---|
| Manual clamp | Simple and inexpensive | Operator variation makes it unsuitable for demanding high-volume cycles |
| Toggle clamp | Fast, repeatable over a fixed stroke | Limited force and poor suitability for changing part heights |
| Pneumatic clamp | Short, consistent actuation time | Needs pressure confirmation and interlock against pressure loss |
| Hydraulic clamp | High force in compact packaging | Leaks and maintenance can stop the cell |
| Swing clamp | Clears the loading path before rotating into position | Requires controlled swing clearance and stroke |
| Electric clamp | Programmable force and position feedback | Higher system complexity; verify force electronically |
Choose the method from required force, access, cycle time, and failure consequence—not from cutting force alone.
Design loading, access, chip control, and maintenance into the cycle
Repeatable loading starts with a fixture built around the entire machining sequence, not just the first cut. Reserve tool access and probe access, then verify clearance for deburring, inspection, cleaning, and part removal. A locator that hides a probe target or traps a cutter forces manual intervention; the lost seconds multiply across a long run.
Use these details to make loading and recovery repeatable:
- Use an asymmetric nest, keyed orientation, and a poka-yoke feature so a reversed part cannot seat; add a part-presence sensor as confirmation, not as the only safeguard against chips or incomplete seating.
- Put chip relief under every seating area, use sloped face geometry, and provide a wiper or accessible cleaning path. Add a coolant purge passage where fluid or chips can collect.
- Treat every quick-change interface as a locating datum: separate it from clamping with a taper pin, pull stud, or zero-point interface. Give it positive seating and a chip-removal path; bolts in clearance holes transfer tightening variation into location.
- Control thermal growth along one direction with a floating locator or relieved contact instead of trapping the hot part.
- Fit a replaceable hardened button, bushing, rest pad, or wear plate at sacrificial contacts, and set replacement limits from measured part error or locator wear—not visual inspection alone.
Log cleaning frequency and locator measurements; stop the run when the defined wear limit or part error is reached, then replace the element.
Qualify the fixture for repeatability, interchangeability, and traceability
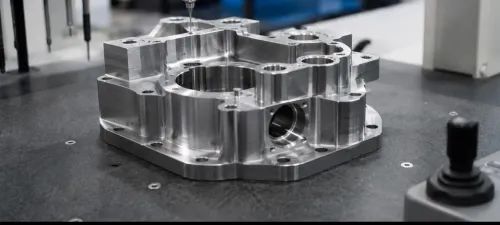
A completed fixture is not qualified because one part measures correctly. Prove its location through repeated loading, interchangeable pallets, duplicate fixtures, drawing revisions, and maintenance. Use a calibrated master artefact or reference part that represents the functional datums, then record the measured feature location against the drawing tolerance.
- Repeatability: load and unload the same reference part through the defined cycle, measuring location each time. Chips and burrs create intermittent outliers; locator drift creates a gradual shift.
- Reproducibility: repeat the test on each pallet or duplicate fixture, then compare the results. This exposes errors in the locating interface that one fixture alone cannot reveal.
- Changeover accuracy: remove and refit pallets, subassemblies, or tooling, then verify location before releasing production.
Set a locator-wear limit from measured part error or a defined wear dimension, not visual appearance. Replaceable buttons, bushings, rest pads, and wear plates let you renew the contact without rebuilding the base; record each repair against a defined inspection interval.
Use keyed interfaces, fixture drawing revision control, and serialized subassembly records to prevent revision-specific hardware from being mixed. This is essential for aerospace traceability. Excellent Tools can include these records with a completed fixture so maintenance can identify the exact configuration in service.
Qualification proves location; it does not prove process capability, which still requires production data and inspection results.
Related product
 | Jig & Fixture A Jigs And Fixtures are workholding gadgets utilized in machining activities as a specialist of help. View product → |
Frequently asked questions
What production data should you calculate before choosing a fixture concept?
Calculate annual volume, takt time, batch size, machine availability, loading time, and machining time. If loading and machining exceed takt time, add capacity, use parallel fixtures, or redesign the operation.
How do you convert a drawing and GD&T into a locating scheme?
Identify the datum feature symbol hierarchy, locate the part from primary, secondary, and tertiary datums, and use only the contacts needed to constrain each degree of freedom. Avoid locating on nonfunctional surfaces unless the process requires it.
How should you size clamps for high-volume machining?
Calculate cutting-force direction and friction at each contact, then provide enough clamping force to prevent movement without distorting the part. Place clamps close to supports and keep them clear of cutting-tool access.
What must you qualify before releasing a production fixture?
Check part repeatability, fixture interchangeability, clamp function, tool access, chip evacuation, maintenance points, and measurement records. Record fixture identification, revision, inspection results, and the parts used for validation.